End-to-End Keychain Manufacturing SOP
From 2D vector concepts to 100,000-unit mass assembly. How Naike controls ±0.01mm CNC mold tolerances, color delta E < 1.0, and 72-hour salt spray durability.
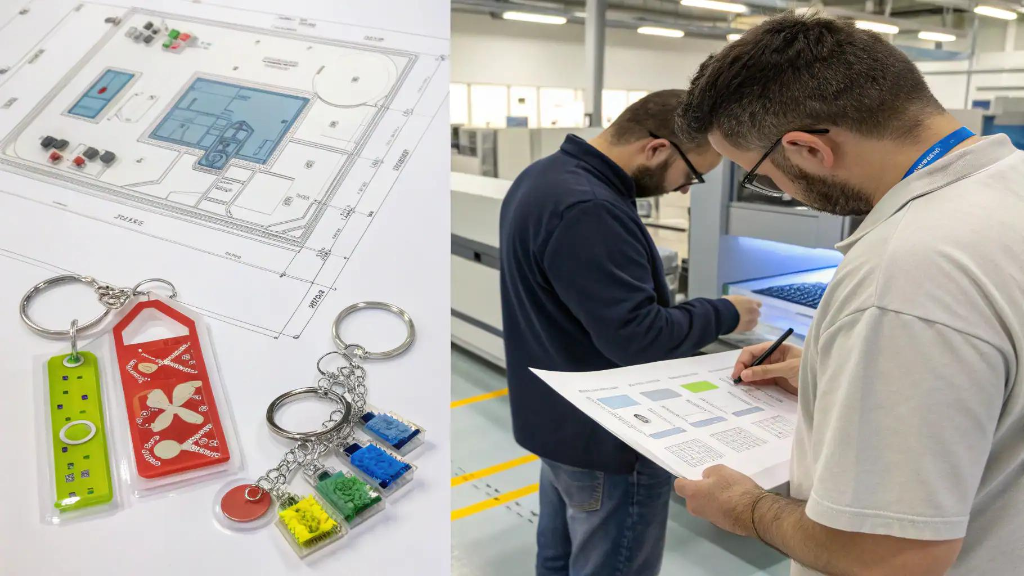
3D CAD & Die-Line Vectoring
Our mold engineers convert client vector files (AI, PDF, DXF) into 3D relief toolpaths. We calculate shrinkage allowance, draft angles (2° minimum for smooth ejection), and enamel cell wall thickness (min. 0.3mm) within 12 to 24 hours.
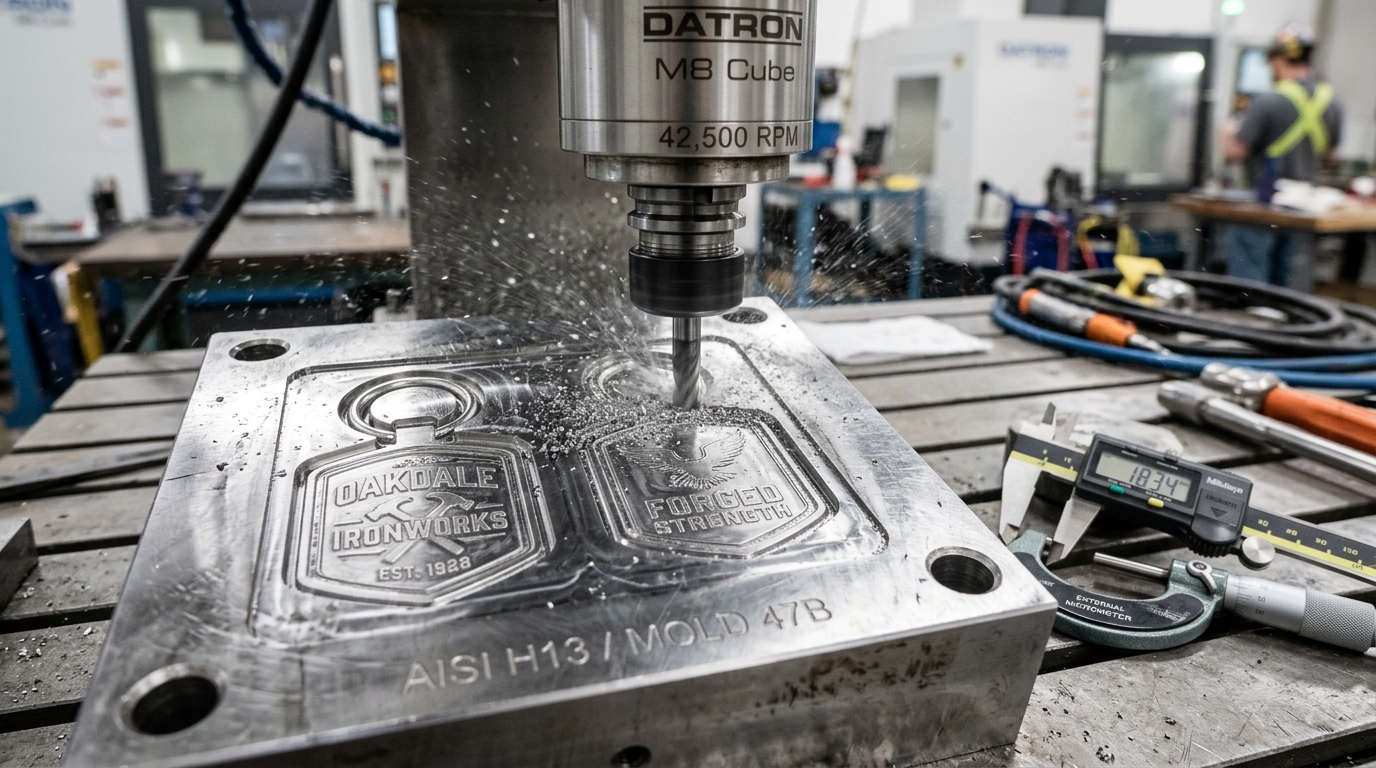
High-Speed CNC & EDM Tooling
Using 15 in-house Beijing Jingdiao CNC engraving machines operating at 24,000 RPM, we carve hardened H13 die steel molds. For micro-details under 0.1mm, mirror-finish electrical discharge machining (EDM) is deployed.
Hot-Chamber Zinc Die-Casting
Zamak-3 zinc ingots are melted at 420°C and injected under 35-50 MPa hydraulic pressure. Rapid solidification in temperature-controlled mold water channels prevents gas porosity and internal shrinkage voids.
Centrifugal Deburring & Polishing
Cast raw emblems undergo centrifugal vibratory tumbling with walnut shells and ceramic media for 120 minutes. All burrs, flash, and parting lines are 100% eliminated, followed by manual wheel mirror buffing.
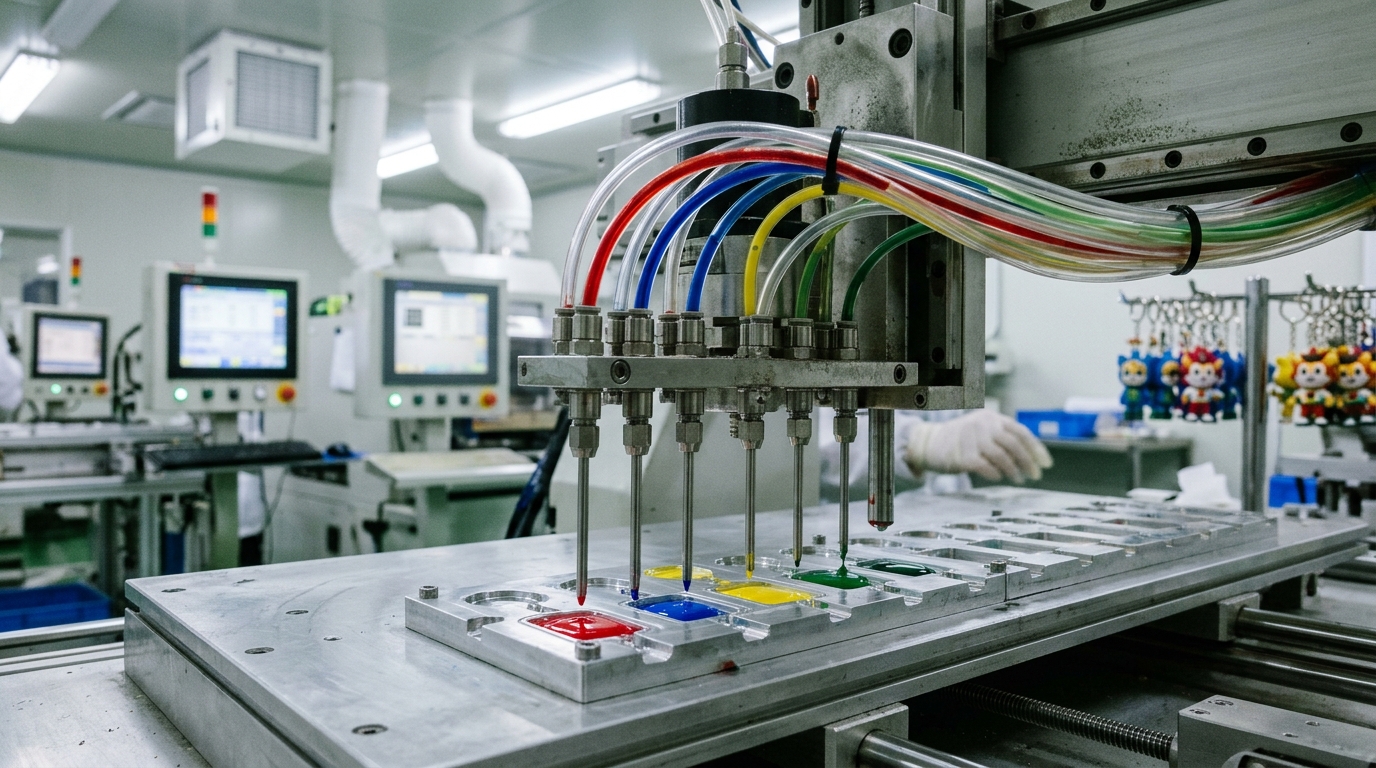
Enamel Dispensing & Stoving
Synthetic paste or liquid enamel is injected into metal cells using automated pneumatic dispensers or skilled hand syringes. High-temp stoving at 160°C ensures cross-linked polymer curing with zero pinholes.
Electroplating & Lacquer Sealing
Emblems pass through rack electroplating (alkaline copper, acid copper, bright nickel, real 18K gold/chrome) followed by an electro-phoretic clear lacquer coat. Cured at 160°C for 30 min, ensuring 72-96h salt spray durability.
Physical Production Infrastructure
Real machinery, real technicians, and verifiable manufacturing square meters in Jinjiang, Quanzhou, Fujian.

Need a Fast DFM Feasibility Assessment?
Send your logo or rough sketch. Our engineering department will evaluate mold draft angles, plating finish feasibility, and deliver a 3D digital sample within 12 hours.
REQUEST ENGINEERING DFM REVIEW →High-Speed Tooling & Automated Production Fleet
Precision machinery engineered for high-volume custom manufacturing: 12-needle automated micro-injection dispensing, 160-ton hot-chamber zinc alloy die-casting lines, and Swiss high-density damask flight tag looms.
15x High-Speed CNC Centers
24,000 RPM spindle speed for carving ultra-fine 3D relief contours into H13 tool steel with ±0.01mm repeatability.
Mold Machining: 12h Fast Turnaround8x LK 160T Hot-Chamber Die-Casters
Real-time hydraulic shot pressure profiling delivering bubble-free, high-density Zamak-3 and Zamak-5 structural castings.
Defect Rate: < 0.08% After Deburring6x Automated Multi-Color Dispensers
Pneumatic sub-millimeter needle metering for 2D/3D soft PVC, eco-silicone, and liquid enamel filling with zero pigment bleed.
Colors: Up to 18 Pantone Shades per Piece12x Swiss Electronic Jacquard Looms
Ultra-fine 50D filament damask weaving for military aviation flight tags with merrowed safety edges and 3M reflective threads.
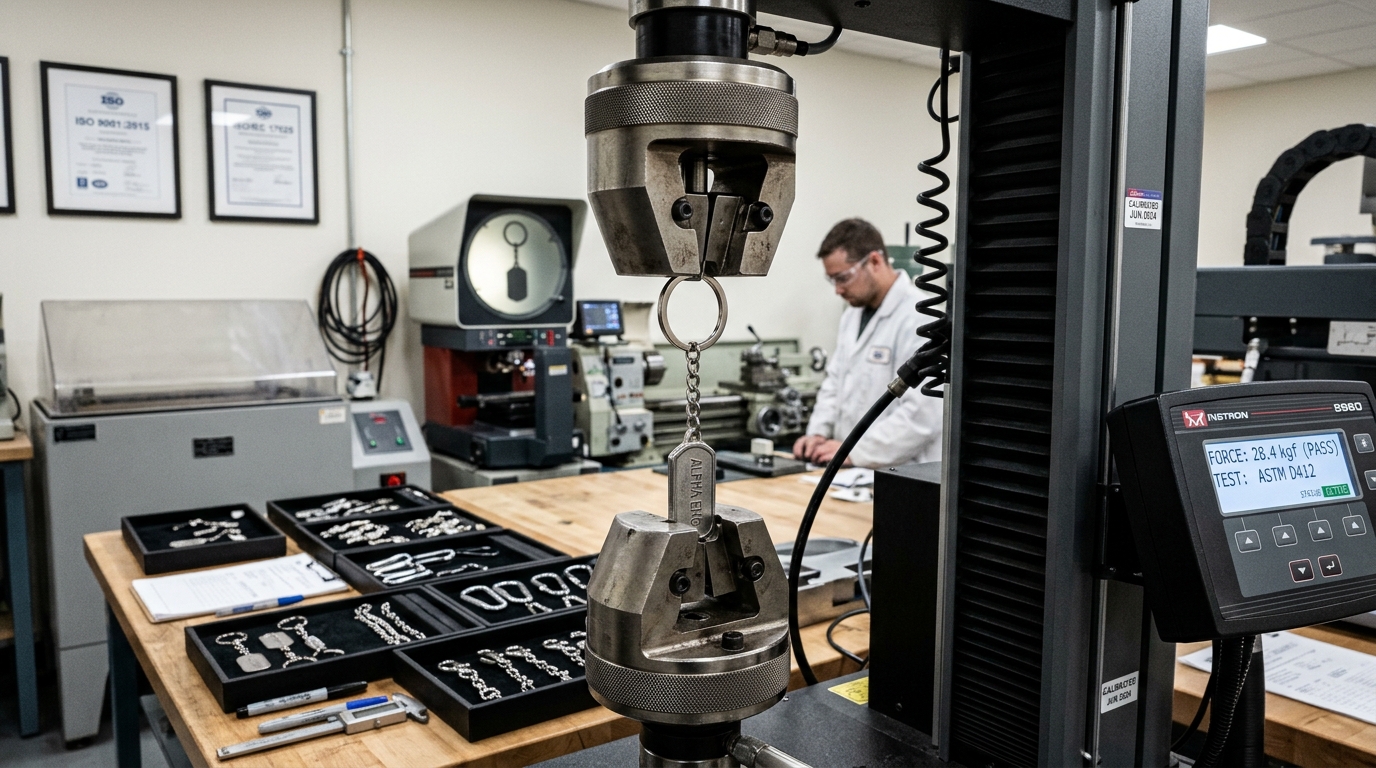
Tensile Strength: ≥ 35 kgf Heavy Duty