1. The Salty Reality of Real-World Keychain Abuse
Few consumer accessories are exposed to a more aggressively corrosive cocktail of environmental hazards than a metal keychain. It spends its working life pressed against sweaty human palms, dropped onto damp winter pavements coated in de-icing calcium chloride salts, left inside humid coastal beach bags, and tossed onto rain-soaked car roofs.
Yet, in the promotional products and commercial hardware market, 90% of keychains are manufactured with nothing more than a superficial 'gold flash'—an ultra-thin electroplated layer barely 0.015 micrometers thick applied directly over a raw zinc alloy or cheap iron substrate with minimal or zero nickel underplating.
What happens next is governed by elementary electrochemistry. Zinc has a standard reduction potential of -0.76 V, while gold sits at +1.50 V. This massive electrical potential difference of 2.26 Volts turns the keychain into a microscopic galvanic battery the moment moisture and salt bridge the two metals through inevitable pinholes in the flash coating. The zinc acts as an energetic sacrificial anode, oxidizing violently beneath the plating skin. Within weeks, unsightly white zinc oxide powders or greenish copper corrosion blooms erupt, destroying the luxury finish.
At Naike, our metallurgical benchmark is uncompromising: every production batch must withstand a minimum of 72 to 96 hours of continuous Neutral Salt Spray (NSS) testing per ASTM B117 / ISO 9227 without a single speck of base metal corrosion. Here is how we engineer that barrier layer by layer.
2. The Anatomy of an ASTM B117 Neutral Salt Spray Chamber
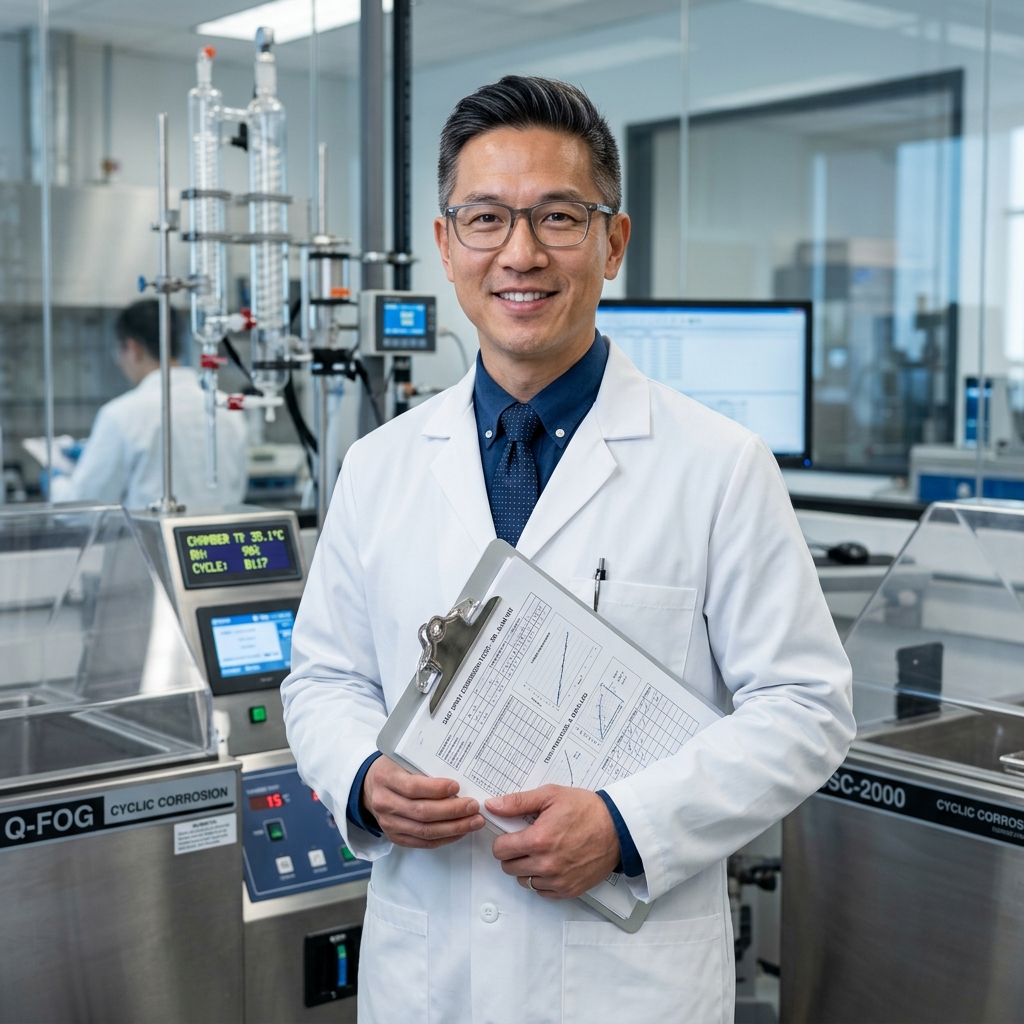
To understand our quality control rigor, let us step inside our on-site environmental test laboratory. The heart of our corrosion assurance is an automated 800-liter ASTM B117 environmental fog chamber.
The testing parameters are rigidly governed by international standards:
Chamber Temperature: 35°C ± 1.5°C constant air temperature.
Salt Solution Chemistry: 5.0% ± 0.5% high-purity sodium chloride (NaCl) dissolved in deionized water with electrical conductivity below 20 μS/cm. The solution must be completely free of copper and nickel contaminants.
Solution pH: Maintained precisely between 6.5 and 7.2 at 35°C. If the pH drifts acidic, corrosion accelerates abnormally; if it turns alkaline, precipitation forms.
Atomization & Fog Fallout Rate: Compressed air at 100 kPa passes through an atomizing nozzle, generating an ultra-fine aerosol fog that collects in calibrated funnels at a rate of 1.0 to 2.0 milliliters per hour per 80 cm² of horizontal collection area.
Test Orientation: Specimen keychains are suspended on non-metallic nylon jigs inclined at 15 to 25 degrees from the vertical, ensuring that condensation runs freely downward across the emblem face without pooling in recesses.
For reference, 24 hours inside an ASTM B117 chamber correlates roughly to one year of outdoor exposure in a mild urban atmosphere, while 72 to 96 hours simulates three to five years of harsh coastal, maritime, and sweaty pocket handling.
3. The Tri-Layer Shield: Copper Leveling, Semi-Bright Nickel, and Bright Nickel
You cannot stop corrosion with decorative gold or chrome alone. Precious metals are too thin and too porous. The true protective shield is built entirely in the preparatory and nickel sublayers.
Layer 1: Alkaline Pyrophosphate Copper (2.0 to 3.0 μm). Zinc alloy is an amphoteric metal that dissolves readily in acidic baths. Therefore, we first deposit an alkaline copper strike to seal the raw zinc, followed by an acid copper leveling bath (8 to 12 μm). Acid copper acts as a ductile micro-filler, flowing into microscopic casting scratches and polishing marks to create an optically flat, mirror-smooth foundation.
Layer 2: Semi-Bright Sulfur-Free Nickel (6.0 to 8.0 μm). This is the unsung hero of industrial corrosion protection. Semi-bright nickel contains zero sulfur (<0.005% S). Because of its high chemical purity, it possesses a noble electrochemical potential.
Layer 3: Bright Sulfur-Bearing Nickel (3.0 to 4.0 μm). Applied immediately over the semi-bright layer, bright nickel contains organic brightening additives that introduce approximately 0.05% to 0.08% sulfur into the crystal lattice, giving it an intense mirror shine.
The Duplex Nickel Magic: The difference in sulfur content creates a controlled potential difference (the STEP test per ASTM B764) of 100 to 140 millivolts between the two nickel layers. If a corrosive pit penetrates the top bright nickel layer, it cannot penetrate downward into the noble semi-bright layer. Instead, the galvanic current forces corrosion to spread laterally across the sacrificial bright nickel layer, protecting the underlying zinc base from penetration for hundreds of hours.
4. The Final Precious Coat: XRF Thickness Calibration
Over the dual nickel shield, we deposit the final decorative metal layer. At Naike, we do not guess plating thickness based on timer dials; we verify every rack using non-destructive X-Ray Fluorescence (XRF) spectrometry per ASTM B568.
The XRF analyzer beams primary X-rays into the keychain surface, exciting secondary fluorescent X-rays whose wavelengths and photon counts precisely identify the elemental composition and thickness of each layer down to 0.001 micrometers.
Our standard plating thickness specifications:
1. Real 18K Gold Plating: 0.06 to 0.12 μm genuine gold alloyed with trace cobalt (0.2% Co) for mechanical hardness (HV 160-200), preventing rapid wear.
2. Bright Decorative Chrome: 0.25 to 0.35 μm hard trivalent chrome over nickel, delivering extreme scratch resistance (HV 850-1000).
3. Gunmetal Black Nickel: 0.5 to 0.8 μm alloyed nickel-tin-zinc composite, producing a sleek modern charcoal aesthetic.
4. Antique Bronze & Antique Copper: Hand-relieved patina over copper, brushed with 600-grit scotch-brite pads to highlight raised 3D contours.
5. The Invisible Armor: Electrophoretic Acrylic Lacquer Sealing
Even the finest gold and bronze electrodeposits contain microscopic atomic-scale pinholes and columnar crystal boundaries. If left unsealed, oxygen and moisture will eventually find a pathway to the substrate.
To achieve our 96-hour salt spray rating, our final production stage deploys automated cathodic electrophoretic coating (E-coating). Keychains are immersed in a water-soluble acrylic-urethane resin bath charged at 45 to 65 Volts DC. The negatively charged metal emblems attract positively charged resin macromolecules, depositing an utterly uniform, pore-free clear polymer skin exactly 8 to 12 micrometers thick over every sharp corner, internal hole, and deep cavity.
The emblems are then transferred to a continuous hot-air convection tunnel and baked at 160°C for 25 minutes. During this thermal stoving, the acrylic molecules thermally polymerize into an impenetrable, crystal-clear ceramic-like barrier. The cured lacquer exhibits a pencil hardness of 4H (ASTM D3363), resistance to methyl ethyl ketone (MEK) solvent rubbing for over 100 double rubs, and complete immunity to salt fog penetration.
6. Autopsy of a Failure: Forensic Analysis of Corroded Competitor Keychains
When prospective clients bring us competitor keychains that failed in their markets, our laboratory conducts a standardized forensic breakdown. The typical failure sequence unfolds in three distinct stages:
Stage 1: Pinhole Rust Formation. The competitor skipped the electrophoretic lacquer to save $0.04 USD per unit. Salt fog directly contacted the 0.015 μm flash gold coating. Within 12 hours inside the ASTM B117 chamber, microscopic black dots appeared where atmospheric salt penetrated through the porous gold crystallites.
Stage 2: Blister Eruption. By hour 24, salt reached the unprotected zinc substrate. Zinc oxide corrosion products occupy approximately 1.5 times the volume of the original zinc metal. This massive volumetric expansion exerted outward hydraulic pressure, lifting the thin copper-nickel plate into raised blisters.
Stage 3: Delamination and Peeling. By hour 48, the blisters ruptured under internal corrosion pressure, allowing salt water to flood beneath the adjacent plating layer. The electroplate flaked off in jagged sheets, exposing raw, crumbling gray zinc alloy.
In stark contrast, our tri-layer nickel plus baked electrophoretic lacquer specimens emerging from the same 96-hour ASTM B117 chamber show zero blisters, zero color shift, and zero flaking, achieving an official ASTM D1654 corrosion rating of 9.8 out of 10.
7. Procurement Specifications: How to Contractually Guarantee 72-96h Salt Spray Pass
Do not accept vague supplier promises like 'high quality plating' or 'anti-rust finish.' Protect your company's investment by writing the following explicit parameters into your B2B master supply agreements:
1. Test Standard: 'All finished keychains must comply with ASTM B117 / ISO 9227 Neutral Salt Spray testing for a minimum of 72 consecutive hours with zero base metal oxidation or blister formation.'
2. Adhesion Verification: 'Plating adhesion must achieve Grade 5B per ASTM D3359 cross-hatch tape adhesion test following 48 hours of humidity exposure.'
3. Thickness Verification: 'Supplier must provide lot-specific XRF thickness measurement certificates confirming minimum 8.0 μm total nickel and 0.06 μm gold / 0.25 μm chrome.'
4. Lacquer Coating: 'Finish must incorporate stoved cathodic electrophoretic clear lacquer with minimum pencil hardness of 3H per ASTM D3363.'