1. The Workshop Floor Reality: Why Enamel Failures Destroy Brand Reputation
In the autumn of 2017, our workshop floor received an urgent warranty claim from a European high-fashion accessories brand. They had procured 35,000 custom gold-plated metal keychains from a local competitor who claimed to supply 'premium cloisonné hard enamel.' Within four weeks of retail delivery in coastal stores across Southern France and Italy, disaster struck. The colored sections began flaking off in tiny brittle chips under everyday pocket contact with car keys. Worse still, the exposed metal recess lines showed ugly greenish oxidation patches where the gold flash had worn away after less than twenty days of rubbing.
When the client flew to our Jinjiang, Quanzhou campus with the failed specimens, our metallurgical laboratory dissected the samples under an optical stereomicroscope. The forensic autopsy revealed two catastrophic engineering shortcuts. First, the competitor had used cheap soft enamel with an unbaked air-cured polyurethane resin rather than high-temperature stoved epoxy paste. Second, to fake the flat, flush look of genuine hard enamel without paying for diamond whetstone manual polishing, they had simply drowned the recessed metal cavities in a thick, convex clear epoxy dome. Over time, friction against key blades micro-cracked the brittle epoxy topcoat, allowing moisture, air, and skin sweat to penetrate directly into the porous zinc substrate.
I share this painful case study because procurement managers frequently ask me the same deceptive question: 'Marcus, both hard enamel and soft enamel look colorful and shiny in catalog photos—why should our brand pay a 25% premium for hard enamel?' The answer lies not in cosmetic appearances on day one, but in the microstructural mechanics of how colored pigments bond with metal lattices, how thermal curing kinetics work, and how planar grinding tolerances affect long-term cyclic wear across three to five years of rough daily handling.
2. Metallurgy and Die-Stamping: The Structural Foundation of Enamel Ribs
Every high-performance metal keychain begins its life in our tooling and stamping department. Whether you specify hard enamel or soft enamel, the initial substrate requires uncompromising dimensional rigidity. We primarily utilize two industrial alloys: H65 high-tensile brass for ultra-sharp coins and luxury tags, or high-purity Zamak-3 zinc alloy for complex 3D sculpted profiles.
When stamping brass blanks under our 300-ton hydraulic toggle presses, the cutting steel die must impart high, vertical cell walls known in the craft as 'metal dam lines' (or cloisons). In genuine hard enamel manufacturing, these metal dividing lines serve a dual mechanical purpose. They physically segregate adjacent liquid pigment pools to prevent color bleeds, and they act as planar sacrificial load-bearing ribs during the subsequent diamond whetstone grinding phase.
In our workshop design rules, we enforce a strict minimum metal wall width of 0.28 millimeters and a minimum cell depth of 0.65 millimeters. If a junior CAD designer attempts to draw hairline dam walls thinner than 0.20 mm, the high hydraulic pressures during stamping will cause the hardened tool steel die to shear off prematurely. Furthermore, during the abrasive grinding cycle, razor-thin metal ribs will curl over under shear friction, dragging microscopic brass shavings across the colored enamel face and causing catastrophic black streak contamination that forces the entire batch into the scrap bin.
In zinc alloy die-casting, draft angles become the primary engineering constraint. While stamped brass allows 90-degree vertical walls, molten zinc injected at 420°C requires a draft angle of at least 1.5° to 2.0° on all cell sidewalls. Without this microscopic taper, the solidified casting will drag against the hardened H13 die cavity upon ejection, galling the metal cloisons and creating microscopic fissures where enamel paste will seep beneath adjacent color sections.
3. Thermal Curing Kinetics: True Cloisonné vs. Modern Synthetic Hard Enamel
Historically, ancient Chinese cloisonné (Jingtailan) employed pulverized silicate glass minerals fused over solid red copper at temperatures exceeding 800 degrees Celsius. While genuine glass mineral cloisonné is extraordinarily hard—registering 7 on the Mohs mineral hardness scale—it suffers from extreme brittleness. If a consumer drops their brass key ring onto a concrete driveway, glass mineral enamel will shatter like fine crystal. Moreover, antique silicate frits cannot reliably replicate modern corporate Pantone color matching, often showing uncontrollable thermal shifts during cooling.
To solve these industrial constraints, our modern engineering standard specifies synthetic hard enamel (often termed imitation cloisonné or epola paste). We formulate our pigments using high-molecular-weight thermosetting synthetic resins blended with fine mineral oxides. The thermal curing cycle is divided into a three-stage programmable furnace curve that guarantees zero internal void formation:
Stage A (Solvent Evaporation): The stamped blanks with dispensed liquid paste enter our conveyor tunnel at 60°C to 80°C for 25 minutes. This gentle gradient allows volatile organic solvents and micro-air bubbles to escape to the surface without blistering or pinhole cavitation.
Stage B (Cross-Linking Polymerization): The temperature is ramped up to 155°C to 165°C and held for 45 minutes. At this critical thermal plateau, the thermosetting resin molecules form tight, three-dimensional covalent cross-links, transforming from a viscous fluid into an impenetrable, rock-hard solid matrix with Shore D hardness exceeding 88.
Stage C (Controlled Annealing): The furnace cooling rate is governed at no more than 3.5°C per minute down to ambient room temperature. This gradual relaxation eliminates internal tensile residual stresses that would otherwise induce micro-cracking during subsequent mechanical grinding passes.
4. The Grinding and Polishing Bottleneck: Where 60% of Production Costs Reside
This is the definitive stage where true hard enamel diverges fundamentally from soft enamel. In soft enamel manufacturing, the metal base is electroplated first, and the liquid enamel is filled into the recesses afterward, sinking down as it dries to leave a pronounced 3D textured ridge. Soft enamel never touches an abrasive wheel after baking.
Hard enamel, in stark contrast, is deliberately overfilled. Our automated dispensers inject excess pigment slurry so that the cured color mounds rise 0.2 to 0.3 millimeters higher than the metal dividing ribs. The entire hardened emblem is then subjected to a rigorous four-step planar abrasive lapping process:
First, coarse carborundum grinding wheels (240 grit) rotate under continuous water coolant, chewing away the excess overfilled mounds until the cured resin and the brass metal ribs form a single, flat, co-planar topography. Second, fine silicon carbide wet-sanding belts (600 grit) remove macro-scratches. Third, automated vibratory lapping with 1200-grit alumina slurry establishes a satin-smooth finish with a surface roughness average (Ra) below 0.25 micrometers.
Finally, the emblems are hand-buffed against high-speed rotating cloth wheels impregnated with green chromium oxide jeweler's rouge. The master polisher must maintain uniform downward pressure of approximately 18 Newtons. If the polisher presses too hard, frictional heat will soften the resin, causing 'pitting drag marks' and over-grinding the thin metal dams. If the pressure is too light, abrasive swirl marks remain visible under calibrated inspection lighting.
To maintain flatness tolerances across thousands of keychains, our tooling department builds custom magnetic nesting fixtures that hold thirty pieces simultaneously against the lapping table. This keeps planar variation within ±0.025 mm across the entire production lot, ensuring that when the keychain is held up to the light, reflections glide across the surface without optical warping or waviness.
5. Electroplating Interface and Chemical Resistance Under Extreme Conditions
Because the hard enamel surface is already ground co-planar with the metal lines prior to electroplating, the final metal finish must be applied over the composite face. Here lies another severe chemical challenge: the cured synthetic enamel resin must resist prolonged immersion in aggressive electroplating chemistry.
Our automated plating line subjects the polished emblems to an alkaline ultrasonic soak cleaner at 55°C (pH 11.5) to remove polishing paste waxes, followed by a mild 5% sulfuric acid electro-activation bath. Substandard resin formulas used by cut-rate factories will leach, soften, or discolor when exposed to acid activation baths. Our proprietary resin formulation undergoes zero discoloration after 30 minutes in concentrated acidic sulfate copper solutions.
During rack plating, a 15-micrometer ductile acid copper foundation is deposited first to level micro-imperfections, followed by 8 micrometers of bright nickel to provide hardness and corrosion barrier protection. The final decorative layer consists of either 0.08 micrometers of genuine 18K gold, mirror-bright chromium, or gunmetal black nickel. Finally, the entire emblem is dipped in water-soluble electrophoretic clear acrylic lacquer and baked at 160°C for 25 minutes to create an impenetrable hermetic seal against salt, atmospheric humidity, and skin acids.
For soft enamel, the sequence is inverted: the blank is electroplated first, baked with lacquer, and then colored. While this avoids chemical bath exposure on the colored areas, the recessed enamel valley cannot be buffed. As a result, soft enamel displays a glossy, meniscus-curved surface that reflects light at multiple disjointed angles, whereas hard enamel displays the singular, monolithic glare of a cut gemstone.
6. Life-Cycle Testing: Tumbling Abrasion, UV Aging, and Thermal Shock
To provide empirical data rather than marketing rhetoric for procurement directors, our quality control department conducted a 3,000-cycle accelerated wear simulation comparing high-grade hard enamel against standard soft enamel keychains:
Test 1 (Tumbling Abrasion Simulation): Keychains were placed in a hexagonal rotating drum containing 20 loose automotive brass keys, stainless steel coins, and dry silica sand at 45 RPM for 72 continuous hours. The soft enamel specimens showed severe rounding of metal ridges, and 14% of the recessed paint pockets suffered color scratching where key tips dug into the soft valley. In contrast, the hard enamel specimens exhibited zero color loss and retained 92% of their specular surface gloss, because the co-planar metal ribs and hardened resin shared abrasive loads equally across the entire surface plane.
Test 2 (UV Accelerated Weathering - ASTM G154): Samples were exposed to UVB-313 fluorescent lamps at 60°C irradiance for 500 hours. The hard enamel inorganic pigments demonstrated exceptional spectral stability with an overall color shift delta E of less than 0.85, whereas non-stabilized soft enamel formulas showed noticeable yellowing (delta E > 3.4).
Test 3 (Thermal Shock - ISO 16750-4): Keychains were cycled between -40°C in an environmental freeze chamber and +85°C in a convection oven with transfer times under 10 seconds across 50 cycles. Thanks to matched thermal expansion coefficients between our modified synthetic resin (alpha = 32 x 10^-6 / K) and Zamak-3 zinc alloy (alpha = 27 x 10^-6 / K), zero delamination or hairline crazing occurred at the metal-resin interface.
7. Procurement Strategy: Deciding Between Hard and Soft Enamel for Your Line
As an engineer who oversees both production bays every day, I never tell clients that soft enamel is inherently 'bad.' It is simply a different industrial tool optimized for different commercial use-cases. Here is our decision framework for brand managers:
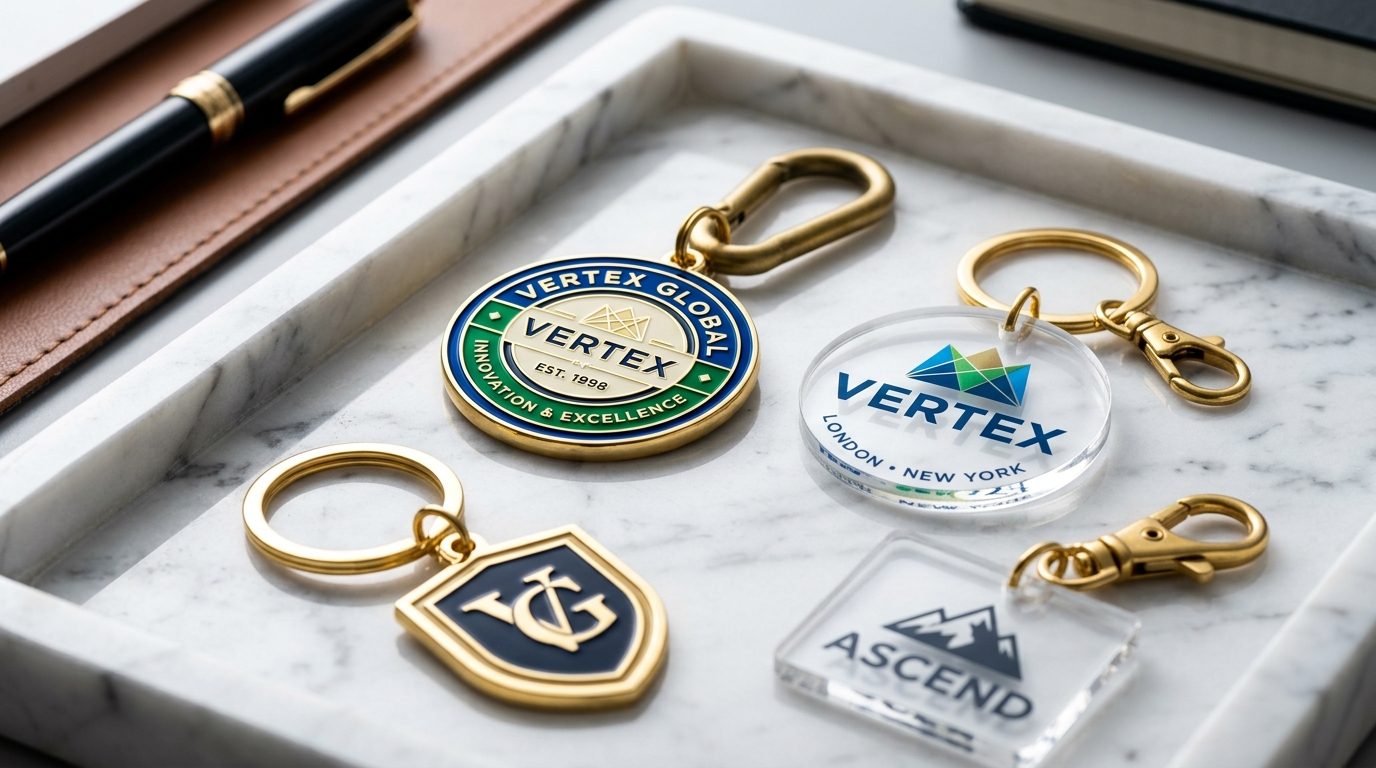
Choose Genuine Hard Enamel when: Your product is an upscale retail merchandise item, an automotive loyalty gift, an airline frequent flyer medallion, or an executive accessory retailing above $15 USD. The smooth, jewel-like flush feel conveys substantial luxury, resists key scratch damage for years, and will never peel.
Choose Die-Struck Soft Enamel when: Your artwork relies heavily on intricate 3D layered contours, stepped metal textures, or steep slopes that cannot be mechanically ground flat. Soft enamel is also the superior choice when unit budget is tight (saving 20% to 30% on labor costs), when quantities exceed 100,000 pieces on short lead times, or when you specifically desire the tactile dimensionality of raised metal wireframes.